Poka-Yoke Training – Error-Proofing Solutions

Why do you need this service?

Poka-Yoke Training teaches teams to design simple safeguards that prevent an error or detect it immediately where it occurs. The method reduces dependence on final inspection, operator memory and warnings alone, supporting quality at source.

When does Poka-Yoke provide the most value?

  • assembly or order-picking errors recur regularly,
  • a non-conformity is detected only at the end of the process or by the customer,
  • work involves many variants and manual decisions,
  • inspection takes time but does not remove the cause of the error,
  • the organisation wants to connect Kaizen, FMEA and standardised work.

The workshop supports the Kaizen system and quality system requirements. We design solutions with the people doing the work, because they know the actual process conditions best.

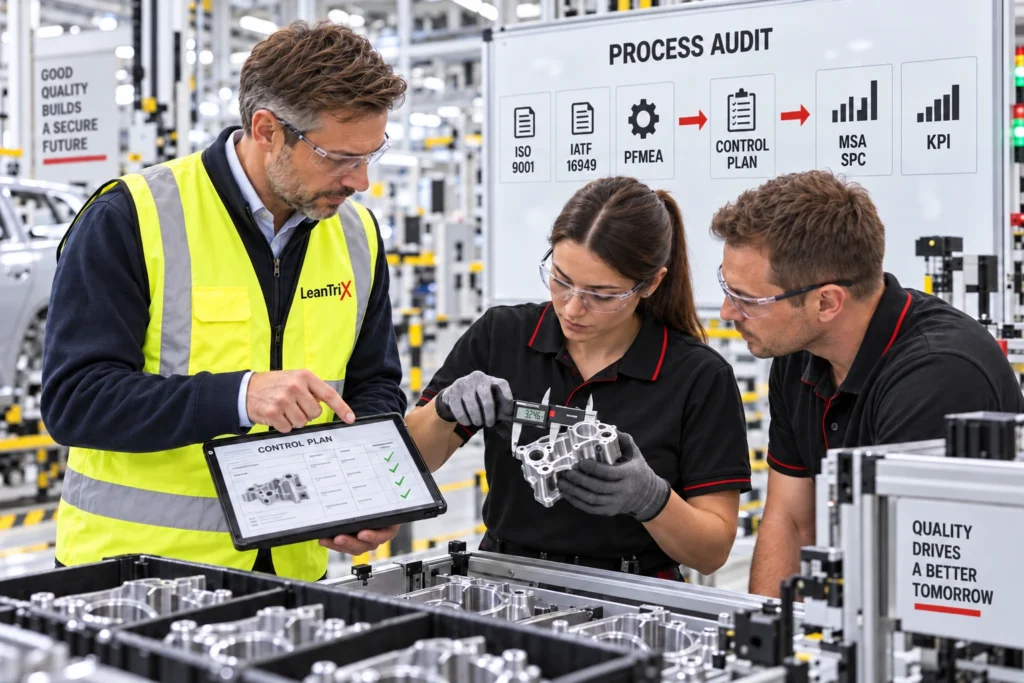
LeanTrix consultant and production team reviewing a process audit, control plan and quality measures.
Szkolenie Poka-Yoke – projektowanie zabezpieczeń przed błędami

What is our role?

We work at the Gemba: observing the process, analysing error types, their effects and causes, then guiding the team through generating and evaluating safeguard concepts. We prioritise solutions that are simple, reliable, easy to check and maintainable.

We can combine Poka-Yoke Training with FMEA, problem solving and TWI. After selecting a solution, we support prototyping, testing, updating standard work and preparing operators and leaders.

Workshop outcomes

  • a list of priority errors and their mechanisms,
  • concepts for preventive and detection safeguards,
  • test criteria and confirmation of effectiveness,
  • a standard for checking Poka-Yoke operation,
  • an implementation and scaling plan.

A handful of facts

0
mechanisms: prevention and detection
0
stages of solution testing through PDCA
0
goal: quality at the source of the process

Implementation support

We provide support based on the Kata process, which allows us to adapt our activities to the specifics of your organization, taking into account the jointly set goals. The Kata process consists of four key elements that enable effective implementation of assumptions.

Determining the course of action

Designing a concept that responds to the organization's goals and challenges.

Determining the current state

Learning about the current situation and collecting input data to define the next step.

Determining the target state

Determining the desired and measurable end result and a plan for its implementation.

Experiments - consultations

Implementation of activities in accordance with the established cooperation model, based on PDCA cycles.

We operate according to PDCA

P

PLAN

PLAN — risk and the purpose of the safeguard

We select a process and an error with a significant impact on the customer, safety, cost or flow. We analyse quality data, observe work and use FMEA and problem-solving logic. We establish whether the safeguard should prevent the error or detect it before it is passed on.

  • selection of a critical problem,
  • description of the error mechanism and the conditions in which it occurs,
  • assessment of existing controls,
  • effectiveness and reliability criteria,
  • a prototype plan and responsibilities.

D

DO

DO — design and prototype

The team develops concepts using shape, sequence, position, quantity, a sensor, an interlock or a simple signal. We build a prototype as quickly as practicable and test it within the actual work cycle, with operators involved.

  • generating several solution options,
  • assessing simplicity, cost and robustness,
  • building a prototype,
  • testing correct and incorrect scenarios,
  • updating instructions and training users.

C

CHECK

CHECK — effectiveness under process conditions

We check whether the safeguard works across all variants, shifts and typical disturbances. We measure the number of errors, process response, false alarms and the ease of daily checks. We collect feedback from operators and maintenance.

  • boundary-condition tests,
  • comparison of quality before and after,
  • checks for bypassing or disabling the safeguard,
  • assessment of the impact on cycle time and ergonomics,
  • a list of necessary adjustments.

A

ACT

ACT — standard, monitoring and rollout

Once effectiveness has been confirmed, we incorporate the solution into the process standard. We define the daily check, the response to a failure and the owner. We transfer effective safeguards to similar products, workstations and processes.

  • approval of the Poka-Yoke standard,
  • a plan for checking that the device works,
  • response to a malfunction or deviation,
  • updates to FMEA and the Control Plan,
  • rollout and a library of good practices.

Want to learn more? Contact us!

    Name and surname *
    Email address *
    Phone number *

    What are you interested in? *

    Additional message (optional)

    * required fields


    Our clients

    Wedel
    Geberit
    Viessmann
    Lajkonik
    Sumito Electric
    Tarczyński
    Autoliv
    Stadler
    UPM Raflatac
    Jost
    BSH
    Danone
    e-obuwie
    Kompania Piwowarska
    Recaro
    Tenneco
    Titanx
    ABM Leantrix Lean Management TWI Toyota Kata TOC
    Amazon Leantrix Lean Management TWI Toyota Kata TOC
    blum Leantrix Lean Management TWI Toyota Kata TOC
    Ikano Leantrix Lean Management TWI Toyota Kata TOC
    Kruk Leantrix Lean Management TWI Toyota Kata TOC
    Lincoln electronic Leantrix Lean Management TWI Toyota Kata TOC
    Sanden Leantrix Lean Management TWI Toyota Kata TOC
    Serpol Leantrix Lean Management TWI Toyota Kata TOC
    Stock Leantrix Lean Management TWI Toyota Kata TOC
    Velux Leantrix Lean Management TWI Toyota Kata TOC

    Our Customers' Opinions