Implementation case study
How operator involvement, red-tag reporting and visual follow-up supported better maintenance performance and career development.
This case describes the implementation and company profile at the time of the original article; historical figures are retained.
Nidec: TPM in the automotive industry (Polish) — an implementation case study. This material draws on the authors’ experience of implementing Lean Management in manufacturing, combining the perspectives of Nidec and a LeanTrix consultant. It shows how to engage operators in Total Productive Maintenance (TPM). The examples can also guide implementation of other Lean methods and tools, including the TWI programme, 5S and SMED.
NIDEC MOTORS & ACTUATORS
NIDEC MOTORS & ACTUATORS (POLAND), based in Niepołomice, belongs to the Japanese NIDEC Corporation, founded in 1973. The source describes it as one of the world’s largest producers of drives and precision drive systems for IT, automotive, aerospace, machinery and other applications.
NIDEC’s main product groups include:
- small precision motors, including motors for hard drives, laser printers, mobile phones, DVD recorders and CD players,
- general-purpose motors: automotive applications including power steering, engine cooling, seat adjustment, door closures and traction; household applications including ventilation, dishwashers and refrigerators; and industrial applications including heat pumps, water heating, lifts, air compressors and power tools,
- machines, including robots and card readers,
- electronic and optical components.
At the reporting point, NIDEC Corporation comprised:
- 14 business divisions,
- 169 subsidiaries in 25 countries,
- 107,500 employees, with 90% based outside Japan.
NIDEC MOTORS & ACTUATORS (NMA) was one of NIDEC’s 14 business divisions. It designs and manufactures electric motors and drives for automotive and industrial applications. Its plants were located in Germany, Spain, China and Poland (Niepołomice), as shown in Figure 1.
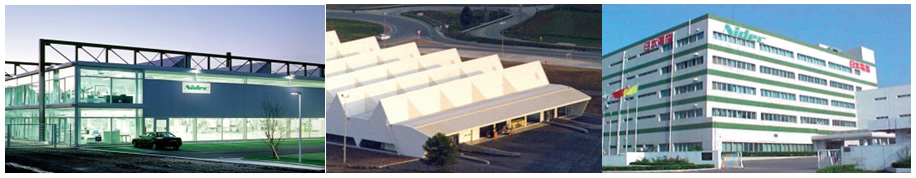
Figure 1. Selected NIDEC production plants. Original figure in Polish.
NIDEC MOTORS & ACTUATORS offered six product lines:
- Braking
- Automotive Closures
- Airflow
- Automotive Seat Adjusters
- Custom Actuators
- Industrial Drives
Figure 2 shows automotive applications of NIDEC MOTORS & ACTUATORS products.
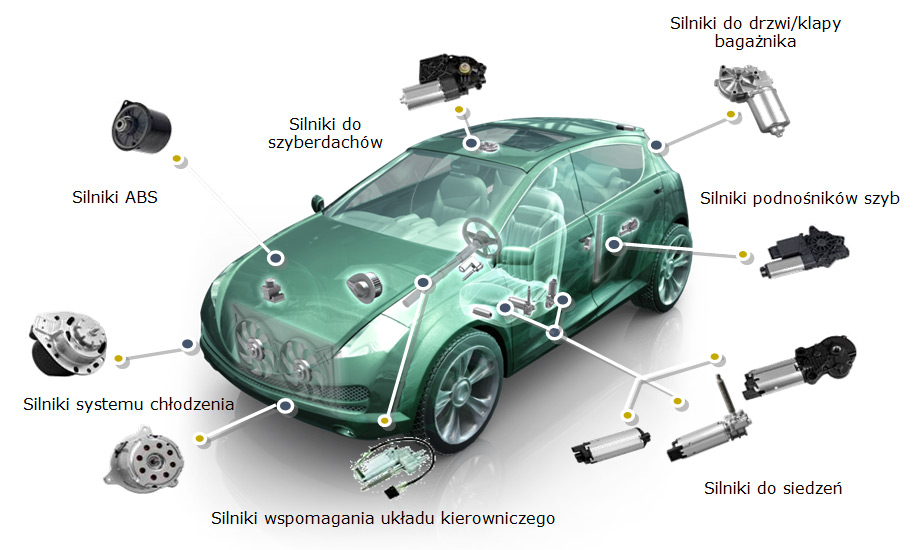
Figure 2. Automotive applications of NIDEC MOTORS & ACTUATORS products. Original figure in Polish.
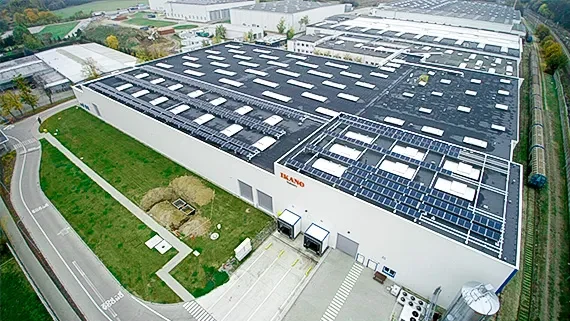
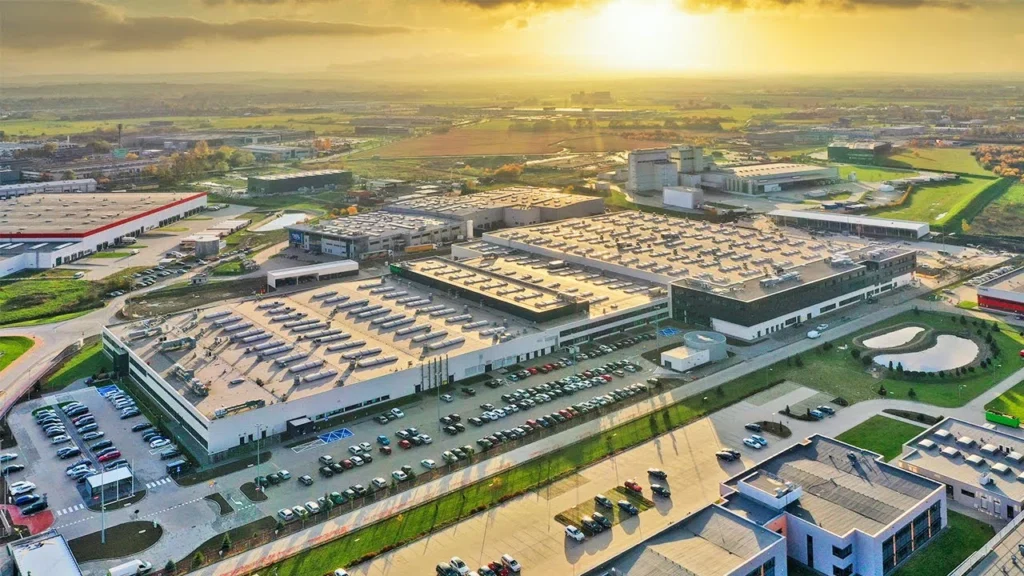
The Polish operation began in 2004 in Zielonki, near Kraków. For its first two years, the plant belonged to the French Valeo Group as Valeo Motors & Actuators. At the end of 2006, that business became part of NIDEC. The decision to build a larger plant in Niepołomice followed, and in 2008 the company moved permanently from Zielonki to its new premises (Figure 3).
The Zielonki plant |
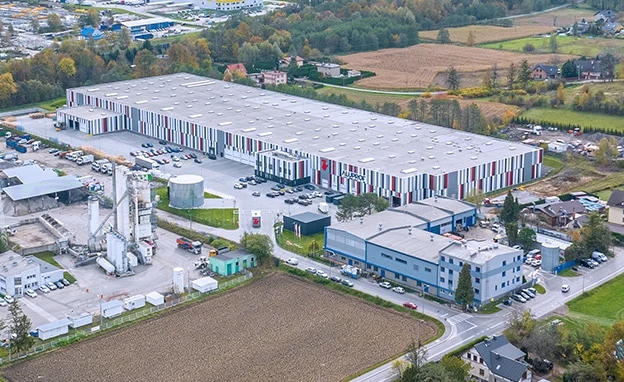
The new Niepołomice plant |
Figure 3. NIDEC production plants in Poland.
At the time described, the Niepołomice plant had 34 production lines, 196 finished-product references, 76 customers and more than 400 employees. Figure 4 presents its main products.
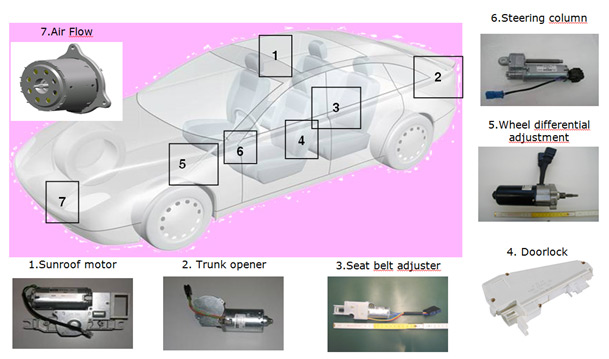
Figure 4. Main products from NIDEC MOTORS & ACTUATORS in Niepołomice. Original figure in Polish.
The source lists ISO/TS 16949, OHSAS and ISO 14001 certifications, reflecting the company’s attention to product quality, employee safety and the environment at that time.
Nidec: areas for Lean and TPM implementation
Many companies assume that employee engagement in Lean Management can be achieved only through financial rewards. Companies introducing employee suggestion systems, often called Kaizen systems, commonly pay for submitted or implemented ideas to encourage improvement. Our experience includes companies receiving dozens of ideas per employee each year and others receiving only a few, even when they pay similar amounts for implemented suggestions. The difference is organisational culture. It develops through everyday involvement in Lean thinking, rather than payment alone. This article focuses on building that culture in areas where operator activity is normal work during the production shift and does not attract extra pay. It therefore does not focus on the suggestion system itself. Once a Lean culture exists, a Kaizen system is more likely to function effectively. Any rewards can then provide additional encouragement rather than the sole reason for participation.
Lean implementation requires operator involvement in areas such as:
- following autonomous maintenance work standards in the TPM programme,
- reporting machine faults,
- reporting and solving production problems,
- following the principles of the 5S system (Polish),
- reporting potential quality defects,
- reporting potential safety incidents (near misses (Polish)),
- following standardised work instructions,
- completing actions arising from audits,
- maintaining the production records needed to update indicators such as OEE.
Developing understanding and engagement in these areas creates strong foundations for an effective Kaizen system and Lean culture. Starting with a suggestion scheme associated solely with payments for activity is likely to make the system fragile.
This article uses TPM to show how to build Lean culture and employee engagement. The approach and implementation principles can also be applied to the other areas listed above.
Engaging employees in TPM at Nidec
Effective implementation and use of TPM tools depend on employee engagement and motivation, particularly among production operators. NIDEC aimed from the outset to create a strong, stable organisation supporting employees’ professional and personal development. An effective business needs involvement in every area. Production operators hold extensive knowledge of machines and the problems encountered in operation. That knowledge must be used for both daily work and process improvement. It is also central to TPM success. Through employee motivation, the team sought to move from traditional equipment maintenance to a modern system based on Lean principles and communication between employees.
The main objectives were:
- maximise equipment effectiveness by eliminating major losses,
- establish autonomous maintenance carried out by operators,
- establish planned maintenance carried out by the maintenance department,
- gain support from management and all employees.
A series of activities was undertaken to achieve these objectives, some of which are described below.
Autonomous maintenance instructions
Work began with clear instructions for inspecting basic machine mechanisms (Figure 5). They were developed for operators and with their involvement. Operator activities were organised into two maintenance levels. The first included checking safety systems such as emergency switches and light barriers, basic inspections and workplace cleaning. The second involved scheduled stops of the entire production line. Maintenance technicians and operators cleaned equipment and inspected each machine’s condition, focusing on critical points. Components requiring replacement were changed where possible. If spare parts or time were unavailable, the issue was recorded on a red card and entered into the electronic maintenance-management system.
Several years earlier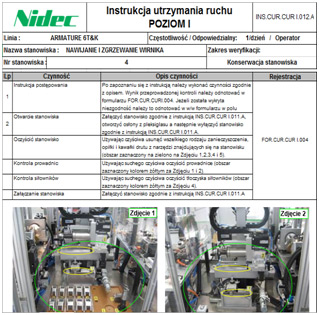 |
At the time of reporting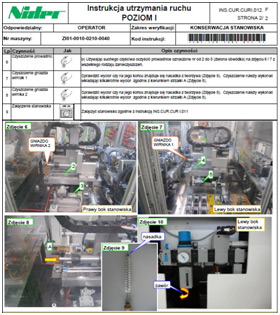 |
Figure 5. An example of an autonomous maintenance instruction. Original documents in Polish.
Instructions are continually improved. When a new problem is found during machine operation, an inspection of that point is added to the routine autonomous maintenance process. Instructions must be clear and easy to read. Most importantly, standards must be created with the people responsible for carrying them out. This is one of the most important ways to engage operators. Whenever an instruction is updated, a maintenance employee trains the production leader, who then transfers the knowledge directly to their team.
Engaging employees in reporting machine problems
A key part of TPM implementation at Nidec was encouraging operators to report problems observed in production. A system was created for reporting issues and tracking resolution. Abnormalities involving machine operation, product quality or safety were recorded on red cards (Figure 6). Their contents were entered into the TPM database and assigned to a person responsible for the work.
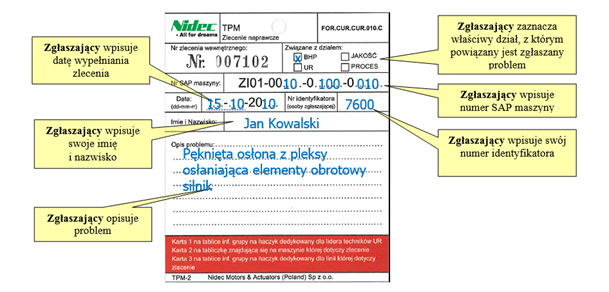
Figure 6. A red card for reporting production abnormalities. Original form in Polish.
Nidec’s red-tag system could work only if everyone expected to use it helped develop it. It could not be designed by the technical department alone. This is a common reason such systems fade in manufacturing companies: operators see another form to fill in and do not understand its purpose. In practice, it improves communication between production employees and maintenance technicians. Operators need to participate in its creation to appreciate that benefit. TPM boards near production lines provide another communication tool (Figure 7).
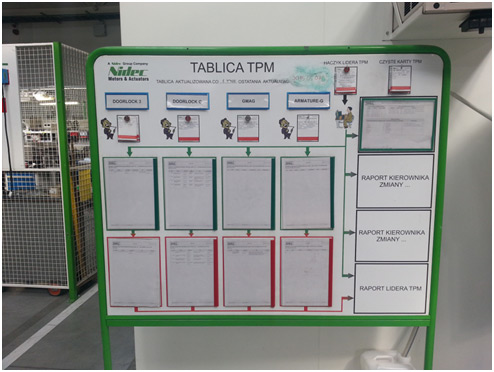 Figure 7. A TPM board. Original board in Polish.
Nidec’s TPM board showed progress on assigned work and the previous week’s breakdown results. Weekly meetings involved the production manager and process engineers. The team reviewed breakdown data and assigned actions. Following the Pareto principle (Polish) , it focused on the three or four dominant problems. The number of jobs reported by each production team was also important: it allowed comparison of operator activity and tracking of trends. Before the boards were introduced, operators complained that they did not know what happened to reported problems, and reporting levels were low. Simple visual management increased participation. The source discusses reports from 2008–2014, while the reproduced reporting chart is labelled 2008–2015. The reports reflect operators’ TPM activity.
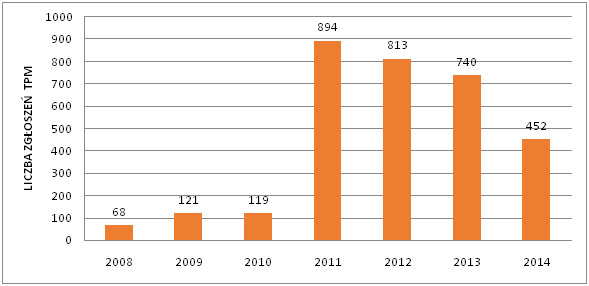
Reported machine problems and faults, 2008–2015. Original chart in Polish; figure numbering follows the source.
This activity was accompanied by a substantial reduction in machine breakdown losses. In 2008, when the reporting system began, breakdowns reduced equipment effectiveness by 3.8%. In 2014, the figure was 1.31% (Figure 9).
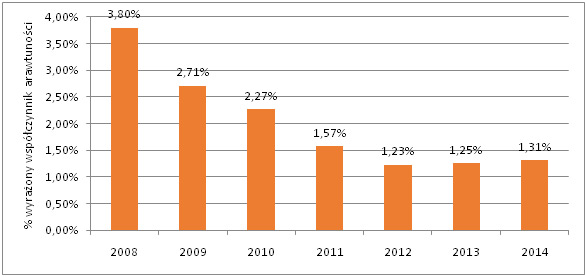
Figure 9. Breakdown losses as a percentage of overall equipment effectiveness. Original chart in Polish.
The case shows a strong association between operators’ involvement in reporting problems and production results, expressed here as lower breakdown losses.
Recognising operators for TPM activity at Nidec
To encourage participation, the most active person was selected each month and received a surprise, non-financial award (Figure 10). Recognition within the team was itself motivating.
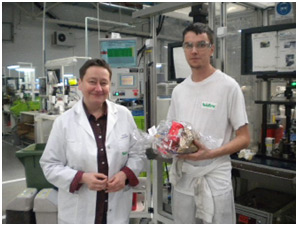
Figure 10. Recognition for TPM activity presented by the head of HR and Production System.
The team looked among the most active operators for people with the potential to become maintenance technicians. Selected employees spent three months in the maintenance department under a technician’s guidance, learning mechanical and electrical repairs. They then gradually began carrying out repairs and inspections independently. At the reporting point, half of the 20-person maintenance team had started as line operators. TPM involvement therefore offered opportunities for personal development and promotion (Figure 11).
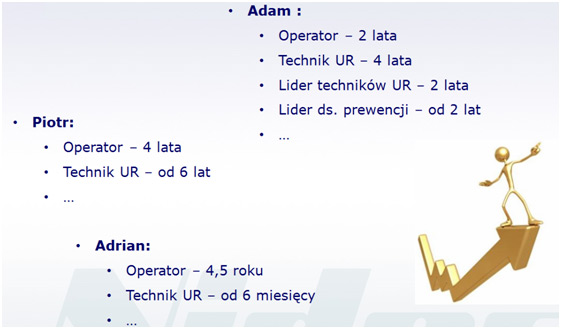
Figure 11. Employee progression at NIDEC. Original figure in Polish.
Communication campaigns and non-financial recognition supported Lean tools and methods. They also helped employees understand that changing company culture requires a change in everyone’s thinking.
Summary: Nidec and TPM
Our practical experience shows that TPM and other Lean methods depend on people and interpersonal communication. Lean culture is built through employees, who follow standards when they understand why those standards matter. Someone encountering TPM for the first time may picture technicians and operators improving machine effectiveness. That is an important part, but successful implementation begins with communication and a sensible division of responsibilities. Employees should be involved in as many implementation activities as possible. Helping people develop solutions themselves is more demanding than giving them finished answers, but it creates the understanding and ownership needed for acceptance.
Employee involvement in Lean Management benefits both the business and its people. The company can gain:
- greater engagement and a sense of equipment ownership and care,
- fewer stoppages and defects, alongside greater operator confidence,
- teamwork that benefits the whole plant,
- a transformation of dirty, disorganised workstations into clean, orderly spaces,
- a better factory image through a well-maintained production floor,
- more opportunity to realise employees’ creative potential.
Employees can gain:
- development through machine-operation training and improved qualifications,
- opportunities to present ideas to management, potentially supporting promotion,
- clean and orderly workstations.
Authors:
Mateusz Danek and Dr Eng. Bartosz Misiurek
I am a promoter of Lean Management and the Training Within Industry program. I am a practitioner. I co-create many startups. Since 2015, I have been the CEO of Leantrix - a leading Lean consulting company in Poland, which, starting from 2024, organizes one of the largest conferences dedicated to lean management in Poland - the Lean TWI Summit. Since 2019, I have been the CEO of Do Lean IT OU, a company registered in Estonia that creates the software etwi.io, used by dozens of manufacturing and service companies in Europe and the USA.